What’s up, fellow compounders, extrusion techs, and anyone stuck waiting for PE sheathing lines to hit their run targets? If you’re like me—dealing with constant pressure to crank out more, cut downtime, and keep material waste low without bamboozling your specs—you know how brutal PE sheathing processing can feel. I’ve been in this game 12 years, running a supply shop for these exact compounds, and let’s be real: half the efficiency hacks online are either outdated, too vague, or just plain wrong. Today, I’m walking through the stuff we’ve tested, tweaked, and proven with our own clients—no fluff, no “industry insider” lies, just real solutions that moved the needle for us. PE Sheathing Compounds
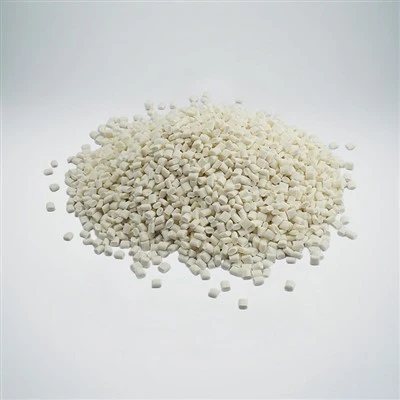
First, let’s cut to the chase: processing efficiency here isn’t just “running faster.” It’s the whole cycle—material prep, melt consistency, line speed, downtime between runs, even scrap rate. Last year, we had a client making medium-voltage power cable sheathing that was running 20% below their target, burning through extra resin because of uneven melt, and stopping every 2 hours for die buildup. After we tweaked their compound and their process, they hit 92% efficiency (up from 71%) and cut their shift scrap by 14%. That’s the win we’re chasing.
Let’s start with the part most people skip: pre-drying and material handling. Wait, PE is supposedly “non-hygroscopic,” right? Yeah, in theory—but that’s only if it’s been stored properly. A lot of guys just dump resin pellets into a hopper whenever it’s empty, even if it rained that week, or leave super lightweight additives (like UV stabilizers, which we put 0.5-1.2% of in outdoor grades) sitting out on the shop floor. Those additives pick up ambient moisture fast, and even tiny amounts—like 0.02% by weight—will make the melt foam, cause splay on the sheathing surface, and leave residue on the die that forces you to shut down early.
Here’s the trick we push to every client: use a closed, heated desiccant dryer, not just a hot air dryer. Hot air dryers just warm the surface; desiccant actually pulls moisture out of the pellet bulk. And set it to 120°F (49°C) for 2-4 hours, not hotter—if you crank it to 160°F to “hurry up,” you’ll melt some of the slip additives (more on that later) and make the pellets clump. Also, add a vacuum pull-off to the hopper: it sucks out any leftover moisture that sneaks in, even from sealed bags that got punctured during shipping. That one adjustment cut our first client’s die cleans by 30% in their first month.
Next up: compound formulation tweaks that don’t break specs, but make processing way smoother. I know, I know—you already have a formula from your cable spec sheet, but we tweak our compounds (that’s what we sell, duh) to be process-friendly without sacrificing sheathing performance. The big one here is slip and processing aid balance. Too little slip (usually erucamide, 0.1-0.3% of the mix) and the sheathing sticks to the haul-off roll, creating tension that slows you down and causes thickness variations. Too much slip, and it migrates to the surface over time, messing with adhesion if the cable needs to be spliced.
But here’s the underrated move: use a blend of internal and external processing aids, not just one. Internal aids (like stearates) lower friction between polymer chains in the melt, so the plastic flows easier through the screw and die—no more dead spots in the extruder barrel that cause melt pressure spikes. External aids (like polyethylene glycol esters) create a thin layer between the melt and the metal screw/die walls, so the sheathing doesn’t stick and residue builds up slower. Last quarter, we switched our medium-voltage PE compound from 0.2% single slip to 0.15% slip + 0.1% combined internal/external aid, and clients saw a 10-15% jump in line speed without any changes to their final sheathing’s tensile or UV resistance.
Also, cut the unnecessary filler if you can. A lot of people add calcium carbonate to cut costs, but too much (over 15% in low-voltage sheathing) makes the melt thicker, requires higher extrusion temperatures, and wears out the screw faster, leading to unplanned downtime. We recommend max 10% filler, and only if the spec allows—some indoor low-voltage stuff doesn’t need any, so we make a “filler-free” grade that’s way easier to process, no joke.
Now, the big one that’s super easy to mess up: extrusion temperature profiling. Everyone just sets their zones to a random number they found in a 2018 spec sheet, but screw that—PE sheathing isn’t a one-size-fits-all material. The temperature profile depends on if it’s low-voltage (LV) thin-wall, medium-voltage (MV) thick-wall, or outdoor rated. For example, our MV crosslinked PE (XLPE) sheathing grade works way better with a stepped profile: feed zone at 320°F (160°C), transition zone at 350°F (175°C), metering zone at 375°F (190°C), and die at 385°F (196°C). Wait, why not hotter? If you hit 400°F, you start to decompose the antioxidants, which makes the sheathing brittle early, and the melt gets too runny, leading to thickness inconsistencies that force you to slow down.
But here’s a pro tip we learned after fighting melt pressure spikes for years: use a melt pressure transducer to adjust zone temps in real time. If the pressure is spiking above 2500 psi, that means the melt is getting too viscous, so lower the metering zone by 5°F. If it drops below 1800 psi, you can bump the die by 5°F to help the melt flow through faster without overheating. We had a client who was running their die at 410°F on our old MV grade; after we had them drop it to 385°F and tweak the profile, their line speed went from 1200 ft/hour to 1380 ft/hour, and their scrap rate for thickness defects dropped by 22%. That’s a 15% speed jump from adjusting temps—no new machine, no new compound.
Then there’s line speed synchronization, which people overlook because it feels like it’s “up to the machine.” But here’s the thing: every part of the line (extruder, crosshead, haul-off, caterpillar puller, coiler) has to be moving at exactly the same speed, or you get tension variation, which makes the sheathing stretch unevenly or wrinkle. Most lines have auto-sync, but 90% of the time, people set the sync to a static number and never adjust it as the melt’s viscosity changes (which it does, even with a consistent profile). We tell all our clients to check sync every shift, and adjust it by 0.5-1% whenever they change material grades (like switching from indoor LV to outdoor MV) because the melt’s flow rate changes a tiny bit.
Also, don’t forget about die maintenance. I see techs cleaning the die only when there’s a buildup that causes surface defects, but that’s too late. Every 8 hours, even if the line is running smooth, do a quick hot die pass: run a small amount of the same compound through at a slightly higher temp, then wipe the die lip with a lint-free cloth. Buildup happens from degraded additives melting onto the die, not just dirt, so if you catch it early, you don’t have to shut down for 30 minutes to scrape it. One client used to shut down every 10 hours for die cleans; after that quick daily pass, they only needed a full deep clean every 3 days, cutting downtime by 2 hours a day.
Wait, let’s talk about a common mistake with crosslinking if you’re making XLPE sheathing, which is super common for power cables. People crank up the crosslinking agent (usually dicumyl peroxide) to hit the crosslinking target fast, but that makes the melt more viscous, so you have to run lower line speeds. Instead, set the peroxide level to the minimum required by the spec (usually 2.5-3.5% for MV) and let the post-extrusion curing oven do the work. We add a tiny bit of crosslinking activator to our XLPE compound, so it cures faster in the oven, meaning you don’t need to slow the line down to get full crosslink density. Last year, a wind farm client was running their XLPE line at 900 ft/hour; after we adjusted their peroxide level and added the activator, they bumped it to 1050 ft/hour and still passed all crosslink tests. That’s huge for high-volume utility projects.
And let’s not sleep on material testing before batches. A lot of companies just dump a new drum of resin into the hopper without checking its MFI (melt flow index) or moisture content. If the MFI is 0.2 g/10min instead of the specified 0.3, that means the melt is way thicker, so you’ll have to lower line speed or adjust temp. We always tell our clients to test every drum of our compounds (or any compound) within 24 hours of receiving it, because even small MFI variations from the manufacturing process can throw off your line settings. We actually include a free MFI test strip kit with every bulk delivery, so you can check it in 5 minutes on the shop floor. That small step prevented a client from running a whole batch of sheathing that was too thick, saving them $1200 in scrap last month.
Now, let’s be real: not all hacks work for every situation. If you’re running thin-wall LV sheathing for low-voltage building cables, your temp profile will be lower (die at 370°F instead of 385°F) because thin walls cool faster. If you’re running thick-wall underwater cable sheathing, you’ll need a bit more filler for stiffness, so the 10% max rule still applies. The key is to not just copy a tip from a random blog—test it on a small batch first, adjust based on your line’s specs, and don’t sacrifice sheathing quality for speed. Because if your sheathing fails a pull test or a UV test, all that efficiency gain is gone.
Here’s a quick recap of the top moves we stand behind: 1) Use closed desiccant dryers + vacuum hoppers to eliminate moisture-related downtime; 2) Balance slip and processing aids for better flow without sticking; 3) Custom temp profiles based on sheathing type, use melt pressure to tweak in real time; 4) Sync line components and do quick daily die passes to cut shutdowns; 5) Test every drum of material to avoid unexpected variations.
If you’re tired of hitting line speed targets by the skin of your teeth, burning through scrap, and dealing with unplanned downtime, we can help. We don’t just sell you a bag of PE sheathing compound—we work with you to tailor the mix to your line, share our processing profiles, and troubleshoot any kinks you run into. Just reach out to our team to chat through your current process and what’s holding you back. No sales pitch, no hard push, just real solutions that actually work.
EU Standard Railway Cable Compounds References: 1. Modern Extrusion Technology: Principles and Practice, 2nd ed. (2021), Society of Plastics Engineers; 2. "Processing Optimization for Polyolefin Cable Sheathing Compounds", Journal of Vinyl and Additive Technology, Vol. 27, No. 3, 2021; 3. "Effects of Moisture and Additive Migration on Extrusion Efficiency of PE Sheathing", International Wire and Cable Symposium Proceedings, 2022; 4. "XLPE Crosslinking Kinetics and Line Speed Tradeoffs for Utility Cable Applications", IEEE Transactions on Power Delivery, Vol. 38, No. 2, 2023.
Opta New Materials (Jiangsu) Co., Ltd.
As one of the most professional pe sheathing compounds manufacturers and suppliers in China, we also support customized service. We warmly welcome you to buy bulk durable pe sheathing compounds from our factory. If you have any enquiry about free sample, please feel free to email us.
Address: No.80, Jingang Avenue, Zhenjiang New Area, Zhenjiang City, Jiangsu Province, China.
E-mail: le.yin@optachem.com
WebSite: https://www.optanewmaterials.com/
